

The Quality Problem in Cat Fountain Manufacturing
Why do some cat water fountain pumps fail at 3 months while others last 3 years?
IQC chemical testing prevents substandard steel bypassing SUS304 specifications.
Eliminates filter seal gaps that leak debris directly into the impeller path.
Catches motors under-delivering flow rates before final casing assembly.
The answer is almost never the pump platform — it's whether the QC system upstream of that pump caught the problems that compress its lifespan: a stainless grade that wasn't SUS304 despite the label, a filter housing gap that bypasses filtration and sends debris to the impeller, a pump that shipped at 70% of rated flow because no flow test was performed before assembly.
Two fountains using identical components can have dramatically different field performance based entirely on whether the manufacturer runs IQC on incoming materials, functional testing at 100% of units, and an independent OQC before shipment.
This guide explains what those stages look like, what specific tests matter for cat fountains, and what questions to ask a manufacturer before placing an order.

The QC Stage System: IQC Through OQC
Manufacturing quality control in China’s pet product factories follows a standardised stage structure. Understanding these stages — and what a factory’s failure to operate any of them means — is the foundation for evaluating a supplier’s quality capability.
QC Stage | Full Name | When It Occurs | What Is Inspected | Who Performs It | Pass/Fail Consequence |
IQC | Incoming Quality Control | Before raw materials or components enter the production line | Stainless steel grade verification, plastic resin certification, pump motor specs, filter media density, electrical component ratings, packaging materials | Factory QC team (independent from purchasing and production) | Failed materials held at goods-in; returned to supplier or quarantined. Production does not begin on non-conforming materials. |
IPQC | In-Process Quality Control | During active production — at defined process checkpoints | Assembly alignment, weld integrity, pump housing seal, flow rate consistency, LED function, surface finish, dimensional accuracy against drawings | Inline QC inspectors stationed at process checkpoints | Defective units pulled from line immediately; process reviewed and corrected before continuing. Prevents defect propagation. |
FQC | Final Quality Control | After full assembly, before packaging | Complete functional test: pump operation, flow rate, noise level, all modes, LED/sensor function, water level indicator, filter fit | QC team; typically 100% of units at this stage for critical functions, AQL sampling for visual/cosmetic attributes | Non-conforming units reworked or scrapped. Only conforming units proceed to packaging. |
OQC | Outgoing Quality Control | After packaging, before shipment | Packaged unit condition, label accuracy, barcode scan, accessory completeness (filters, brushes, cables), carton integrity | QC team using AQL sampling (ANSI/ASQ Z1.4 / ISO 2859-1) | Failed batches held for repackaging or rework. Shipment approval conditional on OQC pass. |
Third-Party Inspection (optional but recommended) | Pre-Shipment Inspection (PSI) by independent body | Typically after 80% of production is complete and 100% of units are packaged | Same as OQC but performed by buyer-engaged independent inspector (QIMA, SGS, Bureau Veritas) against buyer’s specification, not factory’s internal standard | Independent inspector engaged by buyer — critical distinction from factory self-inspection | Failed PSI results in production hold; buyer determines disposition. Independent from factory commercial interest. |

AQL: The Sampling Standard That Determines Whether Your Shipment Gets Inspected Properly
AQL (Acceptance Quality Limit) is the industry-standard framework for statistical sampling in production inspection. It governs two things: how many units from a given batch size are inspected, and how many defects in that sample trigger batch rejection. Most buyers know the term; fewer understand how to apply it correctly for cat fountain manufacturing.
The three defect categories and how they apply specifically to cat water fountains:
Defect Class | Definition | Cat Fountain Examples | AQL Tolerance | Consequence |
Critical | Safety hazard to the cat or user; regulatory non-compliance; renders product unfit for use | Electrical short circuit in pump; pump housing crack that allows mains voltage contact; toxic material in food-contact surface; missing earth connection on mains-connected unit | 0 — zero critical defects tolerated in any inspection | Entire batch rejected and quarantined. Production review mandatory before any further shipment. |
Major | Functional failure that affects product performance; likely to cause returns or complaints; may affect safety indirectly | Pump delivers <60% of rated flow rate; motor noise >40dB when rated <25dB; filter housing gap allowing bypass flow; water level indicator inaccurate by >20%; battery does not hold charge to stated minimum; impeller accessible without tools (safety concern for cats) | AQL 1.0 (tighter than standard consumer goods AQL 2.5) — recommended for cat fountain pump-related defects | Batch held; rework or replacement of affected units before shipment approval. |
Minor | Cosmetic or non-functional; unlikely to affect performance; may affect consumer perception | Surface scratch on stainless lid (outside specification tolerance); minor colour variation in plastic base; label slightly off-centre; packaging scuff | AQL 2.5–4.0 — standard consumer goods tolerance | Batch conditionally accepted; rework if economically viable; documented and disclosed to buyer. |
Product-Specific Tests: What Actually Gets Checked in Cat Fountain Manufacturing
Generic QC checklists describe category-agnostic procedures. Cat water fountains have specific failure modes — electrical, mechanical, material, and filtration — that require product-specific test protocols. These are the tests that separate a QC system designed for this product category from a generic electronics assembly checklist applied to a pet product.

Critical Cat Fountain QC & Verification Protocol Matrix
| Test | Standard / Method | What It Catches | Pass Criterion | Who Should Request It |
|---|---|---|---|---|
| Pump functional test (100% of units) | Factory-defined: run pump at rated voltage for stated period; measure flow rate and noise | Dead-on-arrival pumps; motor winding failures; impeller installation errors; flow rate below spec |
Flow rate within ±10% of rated spec; noise below stated dB ceiling at 1m
|
All buyers — non-negotiable minimum factory QC |
| Hi-Pot (dielectric withstand) test | IEC 60335 / UL 60335 1,500V AC / 1s | Hairline cracks in pump housing insulation; vibration breakdown during transit; wiring pinch points |
No breakdown, arcing, or current leakage above threshold
|
All buyers with electrically-powered fountains (safety compliance) |
| Leak test / water ingress | Factory pressure test or water immersion; IP rating test per IEC 60529 | Pump housing seal failures; tank-to-base seam leaks; battery compartment ingress risk |
No ingress to electronics compartment; zero external leaks under fill conditions
|
Mandatory for wireless/cordless; strongly recommended for all designs |
| Material verification — stainless steel grade | XRF (X-ray fluorescence) spectrometry; magnetic test Alloy Analysis | SUS201 or SUS430 substituted for SUS304; alloy dilution during batch switching |
Cr ≥18%, Ni ≥8% (SUS304 spec); non-magnetic response
|
Buyers specifying 304 stainless (only reliable in-factory check) |
| Food-contact material migration test | LFGB (EU), FDA 21 CFR (US), or EN 1186 3rd-Party Lab | BPA, BPS, heavy metal leaching above limits; non-food-grade resin substitution |
Regulated substance migration below target market statutory limits
|
OEM buyers specifying food-grade plastic; food-safe package claims |
| Noise level measurement | Anechoic / semi-anechoic chamber; IEC 61672 sound level meter | Pump noise above specification; impeller resonance; housing vibration amplification |
dB(A) reading at 1m ≤ stated spec under rated load
|
Brands making quiet claims (<20dB, <25dB on packaging) |
| Battery capacity and cycle test | IEC 62133 / factory-defined performance protocol Wireless Models | Cells below stated mAh; premature degradation; Li-ion protection circuit faults |
Stated capacity maintained; protection kicks in at overcharge thresholds
|
All buyers sourcing wireless/cordless models |
| Drop test / structural integrity | ISTA 1A or ASTM D4169 Transit Simulation | Packaging insufficient for freight; ceramic basin cracks; weld integrity under impact |
Zero functional failure; no sharp edges; no water-contact surface breach
|
Premium buyers, ceramic fountain buyers, retail freight channels |
| Filter housing fit and flow distribution | Factory fixture test: water flow at rated pressure; visual gap inspection | Bypass gaps letting raw water hit pump; loose cartridges; flow channelling |
No bypass gap; uniform flow across medium; seated without force
|
Buyers specifying filtration performance claims |
| Salt spray / corrosion resistance | ASTM B117 / ISO 9227 48–240 hrs exposure | Stainless grade non-conformance; weld seam corrosion; surface coating breakdown |
Zero rust, pitting, or surface degradation within target duration
|
Premium stainless lines; coastal or high-humidity markets |
The Hi-Pot Test — Why It Matters More Than Most Buyers Realise
The Hi-Pot (high potential) dielectric withstand test applies 1,500V AC across the pump’s insulation for one second. Its purpose is to detect hairline cracks in pump housing insulation — damage that is invisible on visual inspection but represents a latent electrical safety failure that can manifest after shipping vibration stress or thermal cycling in the field.
Industry guidance from experienced OEM sources recommends adding the Hi-Pot test as an inline check specifically because hairline pump cracks that only surface after 48 hours of shipping vibration are a documented failure mode in this category. A pump that passes visual FQC and fails in the customer’s home three weeks later due to insulation breakdown is a safety incident — not a warranty claim.

Material Verification: The Gap Between Specification and Production Reality
Material substitution — receiving a material that differs from what was specified — is the most common undisclosed QC failure in Chinese manufacturing, and it is particularly prevalent for stainless steel grade in the cat fountain category. SUS201 and SUS304 appear visually identical. Without IQC material verification, a production run that started on SUS304 can silently shift to SUS201 mid-batch when a sub-supplier’s supply changes.
The Three-Tier Material Verification Hierarchy
Documentation from the steel supplier stating alloy composition. Necessary but not sufficient — certificates can be forged or may not match the specific batch used.
SUS304 is non-magnetic (austenitic structure); a refrigerator magnet should not stick to it. SUS201 and SUS430 are magnetic. Fast, zero-cost, reliable field test — but cannot distinguish SUS304 from other non-magnetic grades.
X-ray fluorescence analysis measures actual alloy composition at the factory. Chromium ≥18%, Nickel ≥8% confirms SUS304. This is the only method that provides definitive grade verification and catches mid-batch substitution. XRF testing adds $50–150 per material batch; third-party lab testing adds $200–400 per sample.
Third-Party Pre-Shipment Inspection: When to Commission One and How
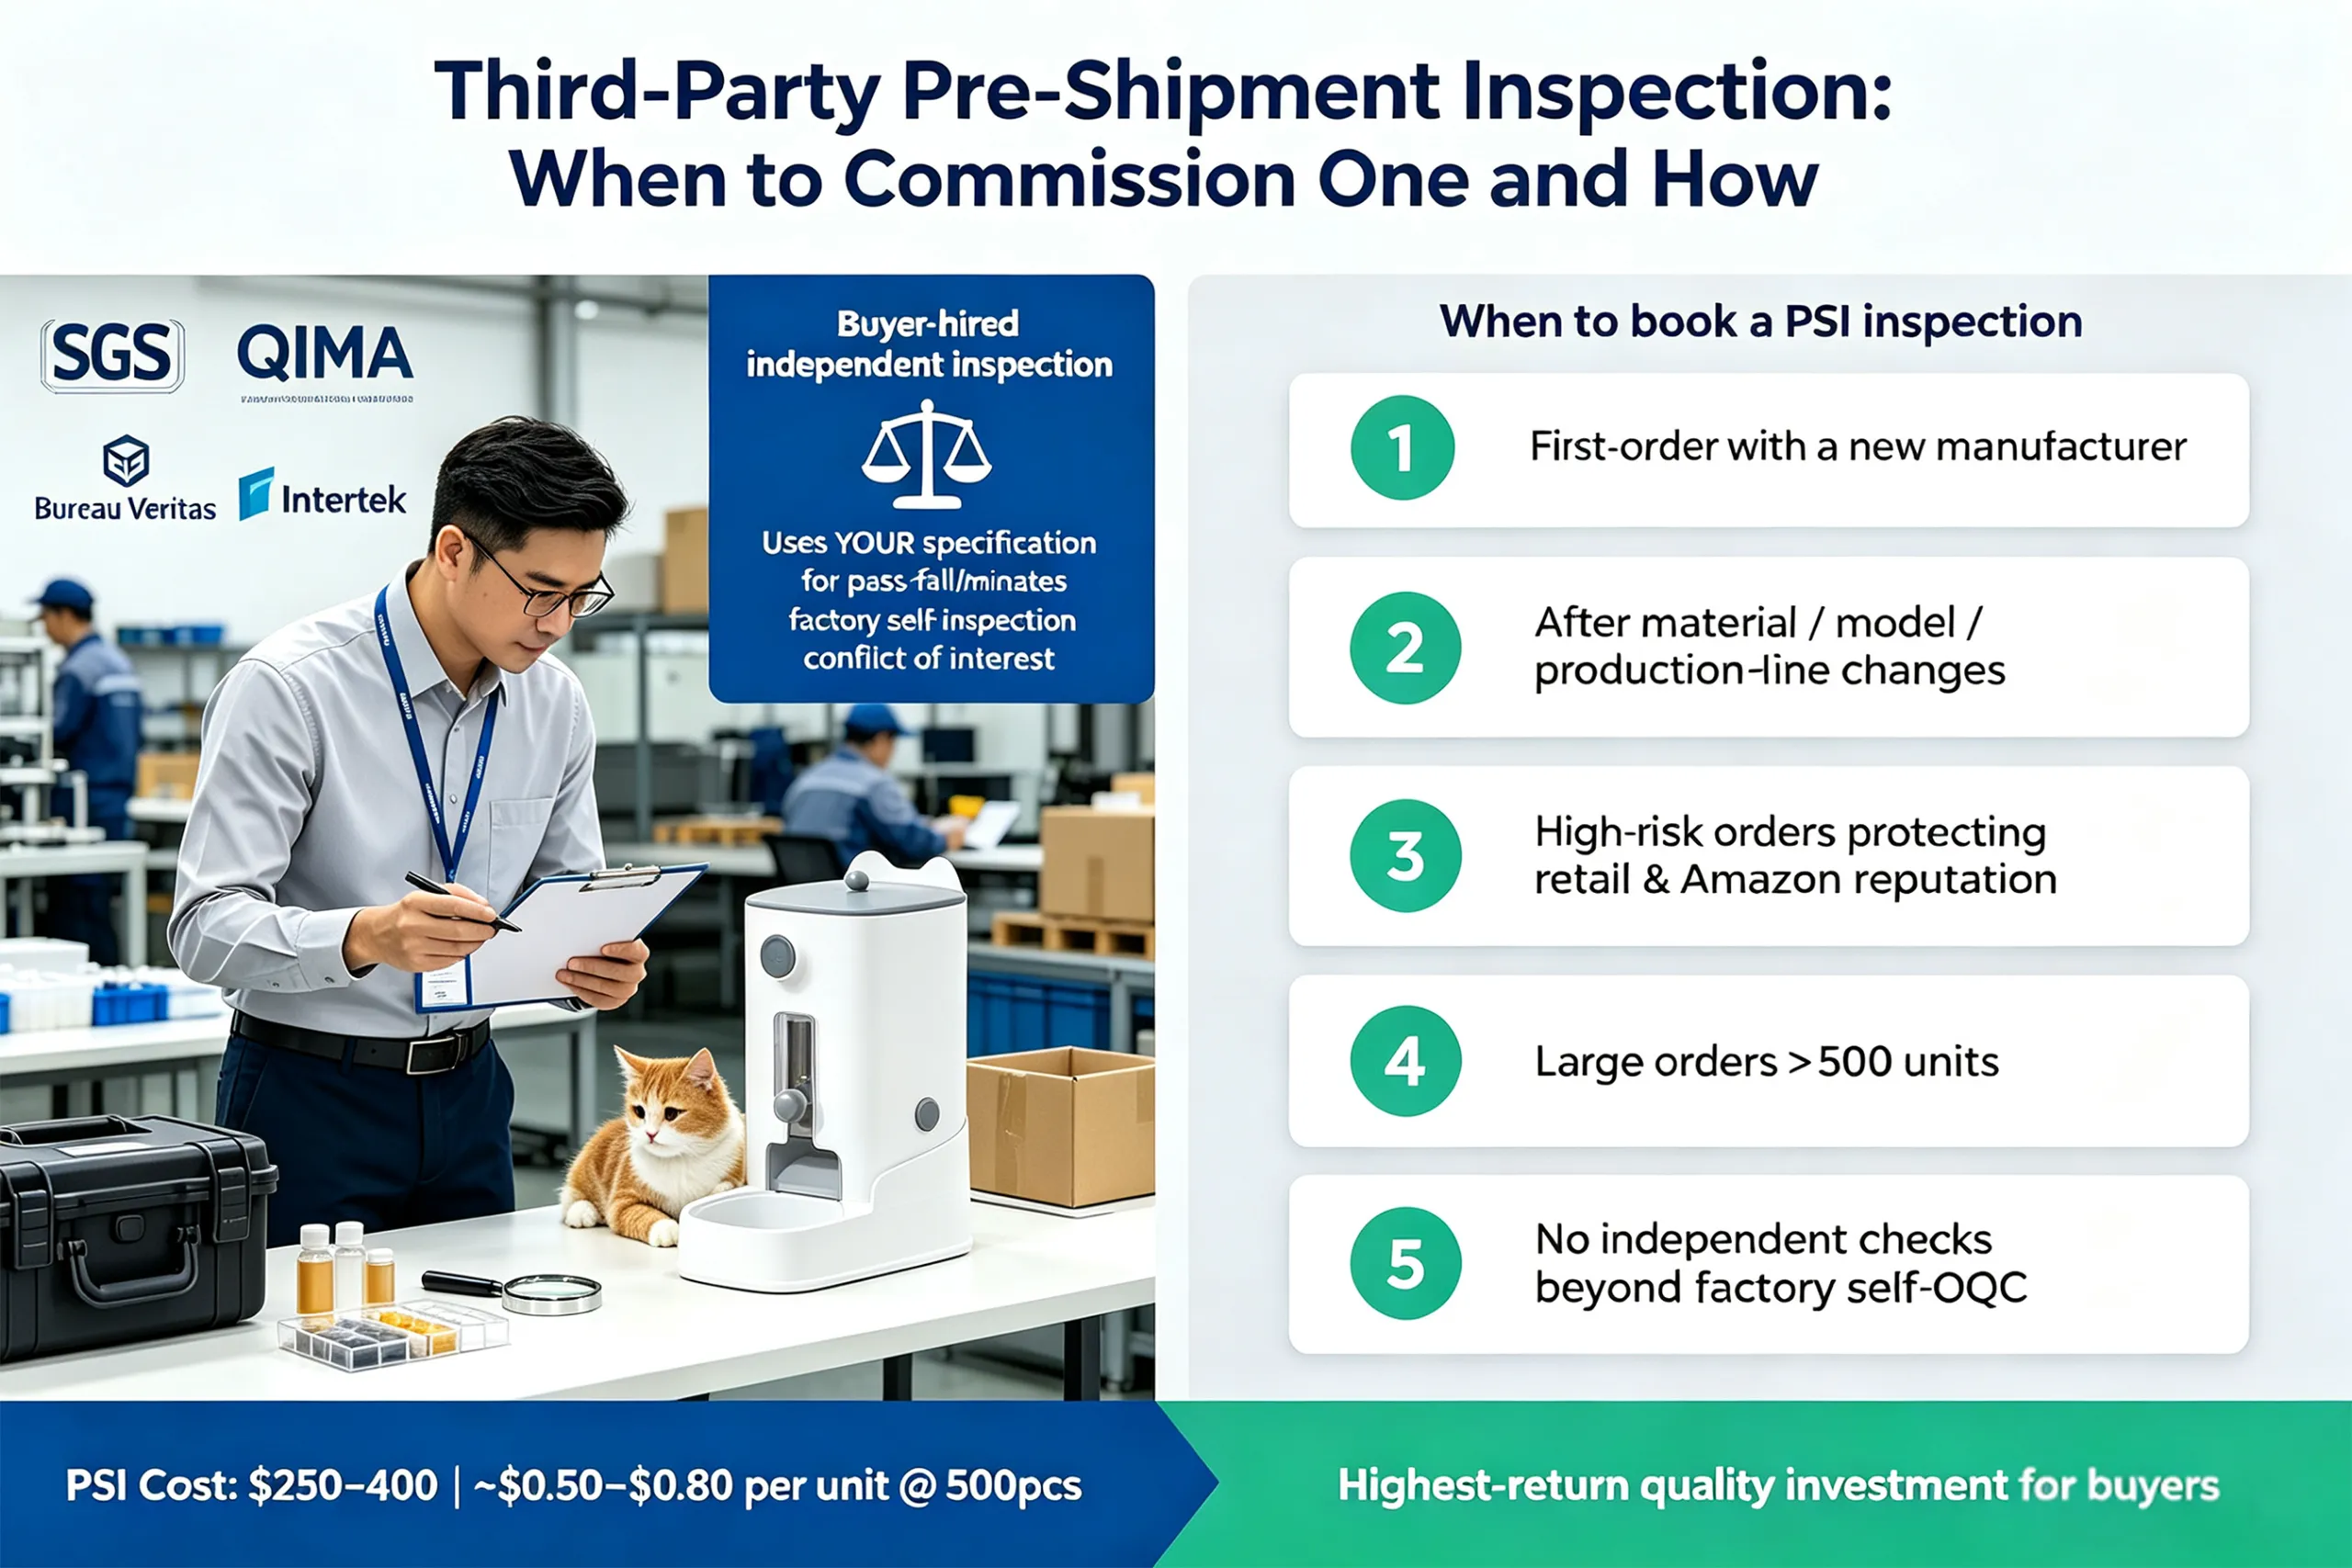
A pre-shipment inspection (PSI) commissioned by the buyer through an independent body — QIMA, SGS, Bureau Veritas, Intertek — is the single most effective buyer-side QC intervention. It removes the self-inspection conflict of interest and applies the buyer’s specification (not the factory’s) as the pass/fail standard.
The Buyer's QC Audit: Questions to Ask Before Placing an Order
A factory that cannot answer these questions specifically — not generically — does not have the QC system required to produce a consistently qualified cat water fountain at commercial scale.
Audit Category | Questions to Ask | What the Answer Reveals | Red Flag |
Factory structure | Is this a factory or a trading company? Can you provide a factory audit report (SGS, Bureau Veritas, QIMA)? | Whether the supplier has actual production control authority or is an intermediary relaying your specifications to an unknown factory | Resistance to factory audit; inability to provide third-party audit documentation; ‘factory visit’ that turns out to be a showroom |
IQC capability | How do you verify incoming stainless steel grade? What documentation do you receive from your steel supplier? | Whether material specification is verified at intake or assumed from supplier claims. XRF verification indicates genuine IQC capability. | ‘We trust our supplier’ without documentation; inability to describe an IQC process; no mill certificate for stainless steel |
Pump testing | What percentage of pumps are tested before assembly? What is your flow rate tolerance? Do you perform Hi-Pot testing? | Whether pump QC is 100% functional screening or AQL sampling; whether electrical safety testing is in the process | Sampling-only pump test (DOA units reach customers); no Hi-Pot test (electrical safety unverified); no stated flow rate tolerance |
AQL standards | What AQL levels do you apply? Who performs your OQC — your own QC team or a third party? Can I commission a third-party pre-shipment inspection? | Whether the factory applies buyer-grade or factory-grade AQL; whether self-inspection creates conflict of interest | Factory claims to use ‘strict QC’ without stating specific AQL levels; resistance to buyer-commissioned third-party inspection |
Material certification | Can you provide LFGB or FDA food-contact test reports for the plastic components? Are these reports for this specific product configuration? | Whether compliance documentation covers the exact product being shipped or the factory’s generic baseline product | Reports that don’t match the specific model being ordered; test reports more than 2 years old; inability to produce documentation within 48 hours |
Non-conformance process | What happens when a batch fails FQC? Can you show me an example NCR (Non-Conformance Report)? | Whether QC failures generate documented corrective action or are quietly reworked without root cause analysis | ‘We don’t have many failures’ without NCR examples; inability to describe a corrective action process; no documented rework procedure |
Production history | Can you provide reference OEM clients for this product category? Are you willing to share production sample approval records from previous projects? | Whether the factory has genuine OEM production history in cat fountains specifically, not just pet products generally | Testimonials only; no verifiable client references; no sample approval documentation from previous projects |
AITAKON's QC System: What 16 Years of Production Learning Looks Like in Practice
AITAKON’s quality control system for cat water fountain production is built around three principles that differ from category-average factory QC: upstream material verification (not downstream defect sorting), functional testing at 100% of units for critical attributes (not AQL sampling of pump performance), and buyer-specified defect classification documented before production begins (not negotiated at OQC stage).
From AITAKON's Manufacturing Practice
Buyers auditing Chinese OEMs in 2026 are scoring suppliers on structured rubrics; failure on any red-line item disqualifies the factory. The non-negotiable items we see in buyer audit frameworks: Hi-Pot inline testing for pump electrical safety; XRF or mill certificate + magnetic verification for stainless grade; 100% flow rate testing before assembly; filter housing fit tolerance in the drawing specification. These are not premium requirements — they are the baseline for a product that will be reviewed on Amazon at scale.
AITAKON's Standard QC Programme for OEM Clients
-
IQC (Incoming Quality Control)
Mill certificate + magnetic screening + XRF verification for stainless steel. Resin certification for all food-contact plastics. Component spec verification for pumps, filters, and electronics before production release.
-
IPQC (In-Process Quality Control)
Inline checkpoints at assembly, pump installation, and seal stage. Dimensional verification against approved drawings at each checkpoint.
-
FQC (Final Quality Control)
100% functional test (pump operation, flow rate, all modes, noise level, water level indicator). AQL visual inspection at Major 1.0 / Minor 2.5 / Critical 0.
-
OQC (Outgoing Quality Control)
Packaged unit sampling at AQL Major 1.0. Label accuracy 100% check. Accessory completeness 100% check.
-
Hi-Pot Electrical Safety
Inline dielectric withstand testing on all electrically-powered fountain models prior to final packaging.
-
Buyer-Commissioned PSI
Supported and facilitated for all production orders; buyer's independent inspector is provided full factory and test floor access.
Frequently Asked Questions
AQL (Acceptance Quality Limit), defined in ANSI/ASQ Z1.4 / ISO 2859-1, determines how many units from a production batch are inspected and how many defects trigger batch rejection. For cat water fountains, the correct AQL specification is: Critical defects 0 (zero tolerance — safety hazards); Major defects 1.0 (stricter than the standard consumer goods 2.5 — appropriate for pump-related functional failures); Minor defects 2.5–4.0 (cosmetic). At a batch size of 2,000 units, General Inspection Level II, AQL 1.0 for major defects: inspect 125 units, accept if ≤2 major defects, reject if ≥3. Specify your AQL levels in the purchase contract before production — most factories default to looser standards unless constrained by buyer specification.
Three methods in escalating reliability: (1) Mill certificate from the steel supplier — necessary but can be forged; verify it matches the batch date and supplier name on shipping documents. (2) Magnetic test — SUS304 is non-magnetic; a refrigerator magnet will not stick to it (SUS201 and SUS430 are magnetic). Fast, free, performed in seconds at the factory. (3) XRF spectrometry — X-ray fluorescence analysis measures actual alloy composition. Cr ≥18%, Ni ≥8% confirms SUS304. Only XRF provides definitive grade verification and catches mid-batch substitution. Request XRF verification in your QC brief for any order where 304 stainless is a product claim.
Yes — unambiguously, for first orders and any order above 500 units. A PSI commissioned through QIMA, SGS, Bureau Veritas, or Intertek costs $250–400 for a one-day inspection covering the full batch. It removes the factory's self-inspection conflict of interest, applies your specification (not the factory's default), and catches functional failures before they become customer returns. At 500 units, the PSI cost adds $0.50–0.80 per unit. A failed shipment that reaches customers — with DOA pumps, incorrect material, or packaging deficiencies — costs an order of magnitude more in returns, replacement, and review damage. PSI is the highest-return QC investment available to a buyer.
Hi-Pot (high potential) dielectric withstand testing applies 1,500V AC across the pump's insulation for one second to detect hairline cracks and insulation weaknesses invisible on visual inspection. These cracks are a documented failure mode — they can pass visual FQC and manifest as electrical safety failures after shipping vibration stress. Most budget cat fountain manufacturers do not perform Hi-Pot testing because it requires dedicated equipment and adds $0.30–0.80 per unit to QC cost. For a safety-conscious brand making electrical safety claims, Hi-Pot inline testing is a non-negotiable QC requirement. Ask prospective manufacturers specifically whether Hi-Pot testing is part of their standard process — and request test records as part of your quality documentation package.
For the US: UL or ETL certification for the power adapter/transformer (electrical safety); FDA 21 CFR for food-contact plastic components; California Prop 65 compliance documentation for sales in California. For the EU: CE marking (LVD + EMC directives for electrical safety); RoHS compliance for electronic components; LFGB certification for food-contact materials; from July 2026, EU Commission Regulation 2024/3190 applies to plastic food-contact materials (bans BPA and several analogues). ISO 9001 factory certification is not product certification but signals a structured quality management system — useful for initial supplier screening. All certification documentation should be specific to your exact product configuration; verify coverage before relying on a factory's existing reports.
Working with AITAKON: Quality-Documented OEM Manufacturing
Complete Quality Transparency on Every Production Run
AITAKON provides full QC documentation for every production run — IQC material verification records, IPQC checkpoint sign-offs, FQC functional test data, and OQC inspection reports — as standard deliverables in our OEM manufacturing package. We support buyer-commissioned third-party PSI on all orders and maintain complete transparency on our QC process.
Request Our QC Documentation Sample Package
Discuss your product's specific testing requirements and compliance specifications with our engineering team.


